
Wuhan Xinglian Trading Co., Ltd.
Precision Rolling & Coil Handling Solutions
Email: support@wuhanxinglian.com Tel: +86 27 8466 9099 | WhatsApp / WeChat: +86 133 8765 8271
Customized rolling lines for copper and brass flat wire in four catalog configurations — from the 5.5 mm inlet draw-roll-draw-take-up line to the 12 mm twin-draw, triple-roll line with online annealing — with finished sections from A 2 mm × B 0.2 mm up to A 16 mm × B 4 mm and line speeds up to 120 m/min.
Copper Flat Wire Rolling Mill Line
The line follows a pulling–rolling–rewinding sequence. Inlet wire of 4–12 mm is paid off, drawn, rolled to the target flat section and rewound. The line is composed of:
-
Wire pay-off decoiling rack
-
Round wire milling machine
-
Precision calender
-
Flat wire milling machine
-
Transversal rewinding (take-up)
-
Electronic control system
-
Cooling system
Process features: pneumatic tension lever speed feedback, spray-type wire die cooling, ball screw traversing, online laser diameter measurement, and pneumatic spool loading and unloading. The drawing, flattening and coiling sections can run independently or inline, and a wheel-type online annealing unit is available as an option.
How the Rolling Mill Line Works
XL-CFW-04 · Precision Type
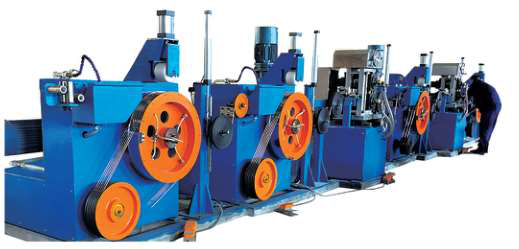
Precision copper flat wire rolling mill line for high-precision, small-specification flat wire production.
XL-CFW-04 · Precision Type
XL-CFW-03 twin-draw, triple-roll line with online annealing.

Large-scale copper flat wire production line with twin drawing, triple rolling and online annealing for high-efficiency production of large-section flat wire.
XL-CFW-03 · Twin-Draw, Triple-Roll, Online Annealing
XL-CFW-02 multi-draw & roll line.

Multi-pass drawing and precision rolling unit for medium-size copper flat wire. Drawing, flattening and coiling can work independently or online.
XL-CFW-02 · Multi-Draw & Roll
XL-CFW-01 draw-roll-draw-take-up line.

The standard layout: pay-off stand, round wire drawing machine, precision rolling mill, flat wire drawing machine, oscillate coiler, electric control and cooling system. Drawing, flattening and winding can run independently or online; online annealing is optional. Features pneumatic tension lever speed feedback, spray-type wire die cooling, ball screw traversing, online laser diameter measurement and pneumatic reel loading and unloading.
XL-CFW-01 · Draw-Roll-Draw-Take-up
Parameter | XL-CFW-01 | XL-CFW-02 | XL-CFW-03 | XL-CFW-04 |
|---|---|---|---|---|
Configuration | Draw-Roll-Draw-Take-up | Draw-Draw-Roll-Draw-Draw-Take-up | Twin-Draw, Triple-Roll, Online Annealing, Draw, Take-up | Draw-Draw-Roll-Draw-Draw-Take-up |
Incoming wire | 5.5 mm | Max 8 mm | Max 12 mm | 4 mm |
Product range | A side 2–5 mm, B side 0.6–3.5 mm | A side 3–8 mm, B side 0.6–5 mm | A side 4–16 mm, B side 2.5–4 mm | A side 3.5–8 mm, B side 0.2–2.2 mm |
Max line speed | 120 m/min | 120 m/min | 80 m/min | 120 m/min |
Roller diameter | 200 / 180 mm | 250 mm | 350 / 300 / 300 mm | 180 / 160 mm |
Capstan diameter | 600 mm | 800 mm | 1200 mm | 650 mm |
Idler diameter | 300 mm | 400 mm | 400 mm | 400 mm |
Auxiliaries | Roller cooling, drawing cooling, electric control | Roller cooling, drawing cooling, electric control | Roller cooling, drawing cooling, electric control | Roller cooling, drawing cooling, electric control |
Total power | 65 kW | 140 kW | 450 kW | 80 kW |
The copper flat wire rolling mill line is available in four configurations, with catalog model codes XL-CFW-01 to XL-CFW-04. Each configuration has its own published specification.
Technical Specifications — Four Catalog Configurations
-
Copper and brass flat wire production for the cable and electrical industry
-
Copper busbar manufacturing
-
Enamelled wire and enamelled flat wire production (magnet wire)
-
Flat wire for further winding operations, taken up on the moving disk transversal rewinder and paired with the XL-OR oscillate recoiler series
Where the copper flat wire rolling mill line is deployed.
Applications
PLC with touch screen and a dedicated electrical control system coordinate the complete line.
Integrated control
05
Ball screw traversing at ±0.1 mm, with pneumatic spool loading and unloading to reduce handling.
Precision winding at the take-up
04
Drawing, flattening and coiling can run independently or inline, and online annealing is available as an option.
Flexible operation
03
Pneumatic tension lever speed feedback stabilizes the drawing and rolling sections.
Closed-loop tension control
02
Online laser diameter measurement and spray-type wire die cooling keep flat wire dimensions in tolerance during continuous running.
Inline measurement and cooling
01
Five characteristics based on the real line design.
Why Choose the Copper Flat Wire Rolling Mill Line
The line is designed for copper and brass flat wire, copper busbar, enamelled wire and enamelled flat wire. Incoming wire and finished sections depend on the configuration — for example, the XL-CFW-01 takes 5.5 mm inlet wire to A 2–5 mm × B 0.6–3.5 mm, while the XL-CFW-03 takes up to 12 mm inlet wire to A 4–16 mm × B 2.5–4 mm. For other materials, submit your specification for review by our technical team.
Maximum line speed is 120 m/min on the XL-CFW-01, XL-CFW-02 and XL-CFW-04 configurations, and 80 m/min on the large-section XL-CFW-03. Actual running speed depends on the inlet wire size, the target flat section and the selected roll diameter.
The standard layout includes a wire pay-off decoiling rack, round wire milling machine, precision calender, flat wire milling machine, transversal rewinding, electronic control system and cooling system. Optional equipment includes a wheel-type online annealing unit.
Yes. The drawing, flattening and coiling sections can operate independently or inline. This allows the line to be used for single-process work, such as rewinding only, or as a complete draw-roll-draw-take-up line.
The line uses online laser diameter measurement to monitor the flat wire during running, combined with spray-type wire die cooling and pneumatic tension lever speed feedback to stabilize the process. Rolls are available in 160, 180, 200, 250, 300 and 350 mm diameters.
Roll and capstan diameters are matched to the configuration: for example, the XL-CFW-01 uses 200/180 mm rolls with a 600 mm capstan, the XL-CFW-03 uses 350/300/300 mm rolls with a 1200 mm capstan, and the XL-CFW-04 uses 180/160 mm rolls with a 650 mm capstan. Share your product range and we will confirm the suitable configuration.
Total power depends on the configuration: 65 kW for the XL-CFW-01, 140 kW for the XL-CFW-02, 450 kW for the XL-CFW-03 and 80 kW for the XL-CFW-04, each covering the complete unit with its electrical control system. All configurations are operated through a PLC with touch screen.
Yes. A wheel-type online annealing unit is available as an option, used in the twin-draw, triple-roll configuration for large-section flat wire production. Include your annealing requirement in your inquiry so we can confirm the configuration.
The take-up end uses moving disk transversal rewinding with ball screw traversing and pneumatic spool loading and unloading. The winding principle matches our oscillate recoiler series, which offers spools from PN400 to PN800 mm and servo constant-tension control.
Quotations depend on the configuration — standard draw-roll-draw-take-up, multi-draw and roll, twin-draw with online annealing, or precision type — plus selected roll diameters and options. Send your inlet size, target section and required layout to manager@wuhanxinglian.com for a proposal.
Common questions on materials, speed, layout, options and quotations.